Wheel Inner Rings
Product ID: 10513
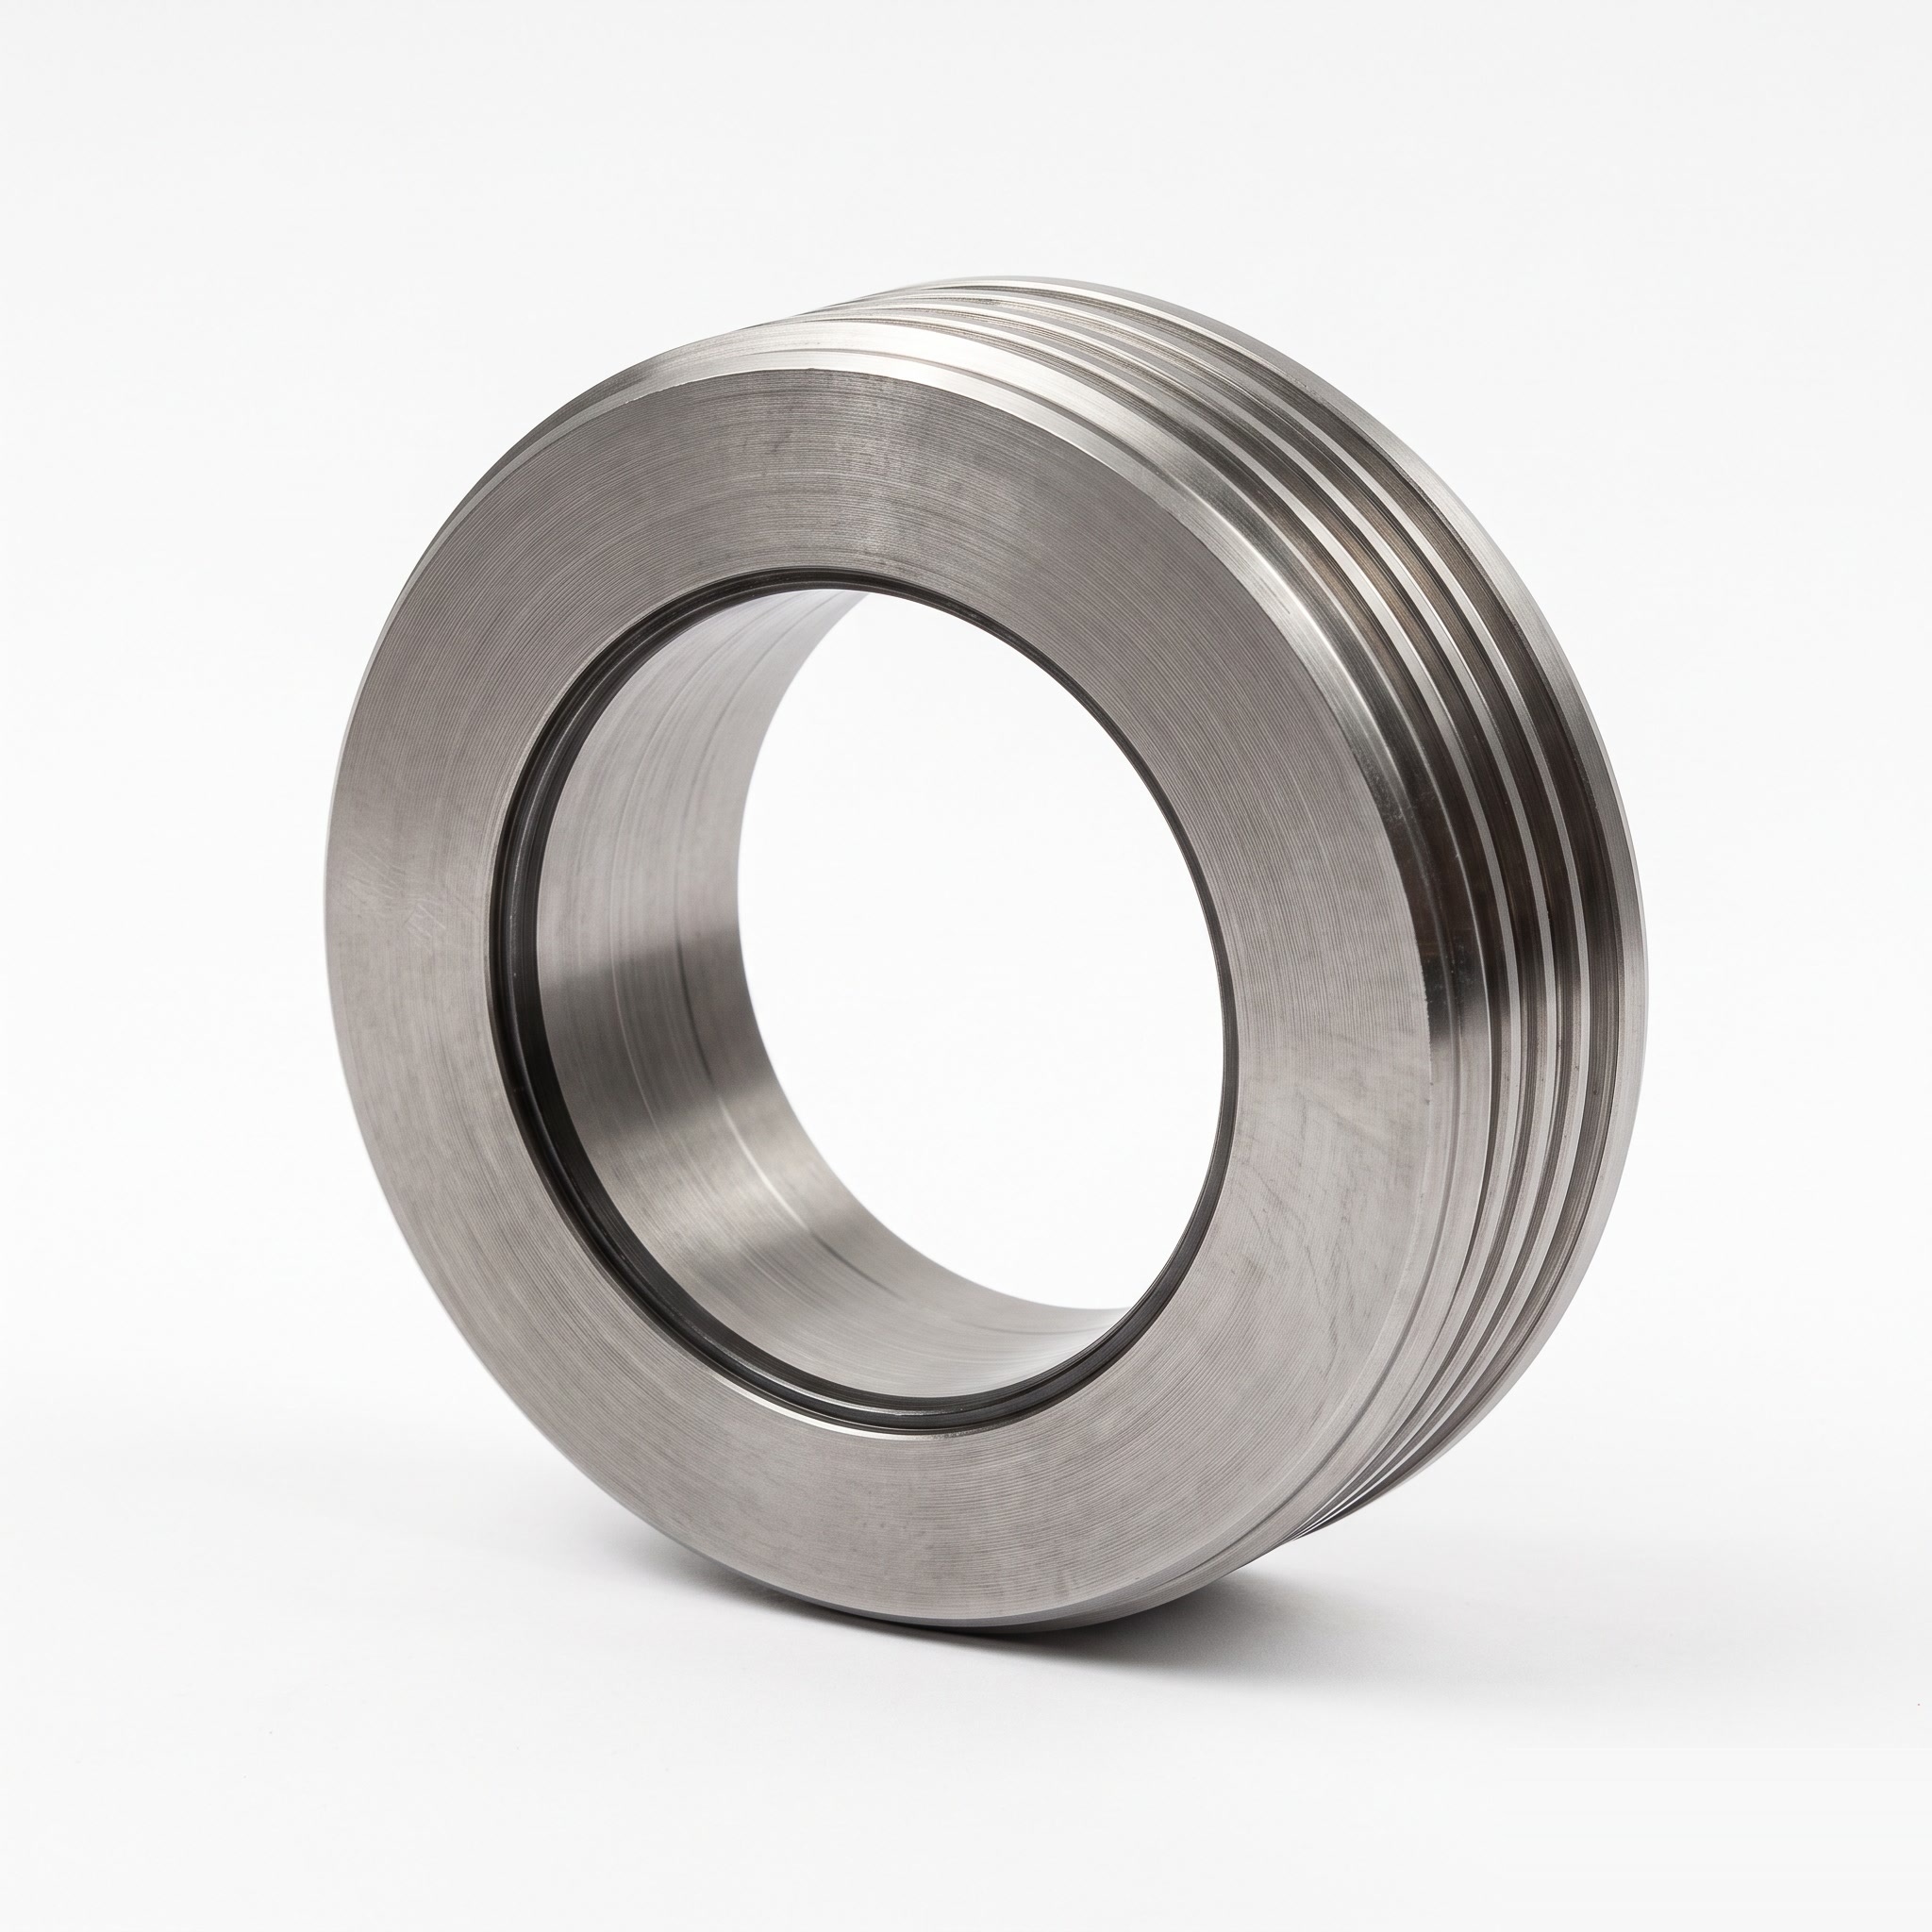
Custom machined wheel inner rings with a central bore, stepped faces and circumferential grooves for drawing-defined locating and mating interfaces.
Product Description
These annular components provide a compact interface between concentric parts in a customer-designed wheel assembly. The bore establishes the radial fit, while stepped faces can provide axial seating surfaces. Circumferential grooves are matched to the mating design; their purpose and profile must be specified rather than assumed. Bore-to-outside runout and face alignment are important where the ring rotates or locates another component. Application examples, subject to assembly design: concentric wheel subassembly location or a spacing/seating interface around a hub. A diameter check alone does not establish rotational accuracy. The datum axis and the face used for axial seating should be identified so that groove position, radial runout and face wobble are evaluated in the same reference system.
Product Features
Central bore for radial location. Stepped faces for axial seating where required. Circumferential groove geometry matched to adjoining parts. Drawing-defined control of runout, face parallelism and edge condition. Engineering focus: separate control of locating diameter and rotational runout.
Technical Specifications
Indicative custom specification for RFQ; final drawing and quotation govern. Materials: 1045 / 4140 steel or 304 stainless steel; grade and condition selected by the wheel design. Tolerances: Proposed: selected diameters +/-0.02 mm; face/radial runout 0.03 mm to a defined datum. General metal sizes: ISO 2768-1-m if adopted. Surface treatment / roughness: Steel: black oxide + preservative; stainless: passivation. Marked seating faces Ra max. 1.6 um before treatment. Indicative size range: OD 30-150 mm; bore 15-100 mm; width 8-40 mm; bore smaller than OD with drawing-defined wall section. Proposed process: Blank cutting / CNC turning/boring/grooving / drilling if required / deburring / treatment / runout inspection. MOQ: Reference lot 100 pcs per part number; final MOQ per quotation. Target lead time: Target 2-3 weeks (10-15 working days) after drawing/material/order approval; final quotation governs. Reference standards: ASTM A29/A29M; ASTM A276/A276M; ISO 1101:2017; ISO 21920-1:2021; ISO 11408:1999; ASTM A967/A967M; apply only to the selected material/process and scope. Note: Groove purpose and material strength are project-specific; this is a locating-ring proposal, not a bearing-race rating. Size-range limits are not all combinable. Surface/heat treatments are project-managed through qualified partners where required.
Related products
More from New Energy Vehicle Parts
Steering Bases
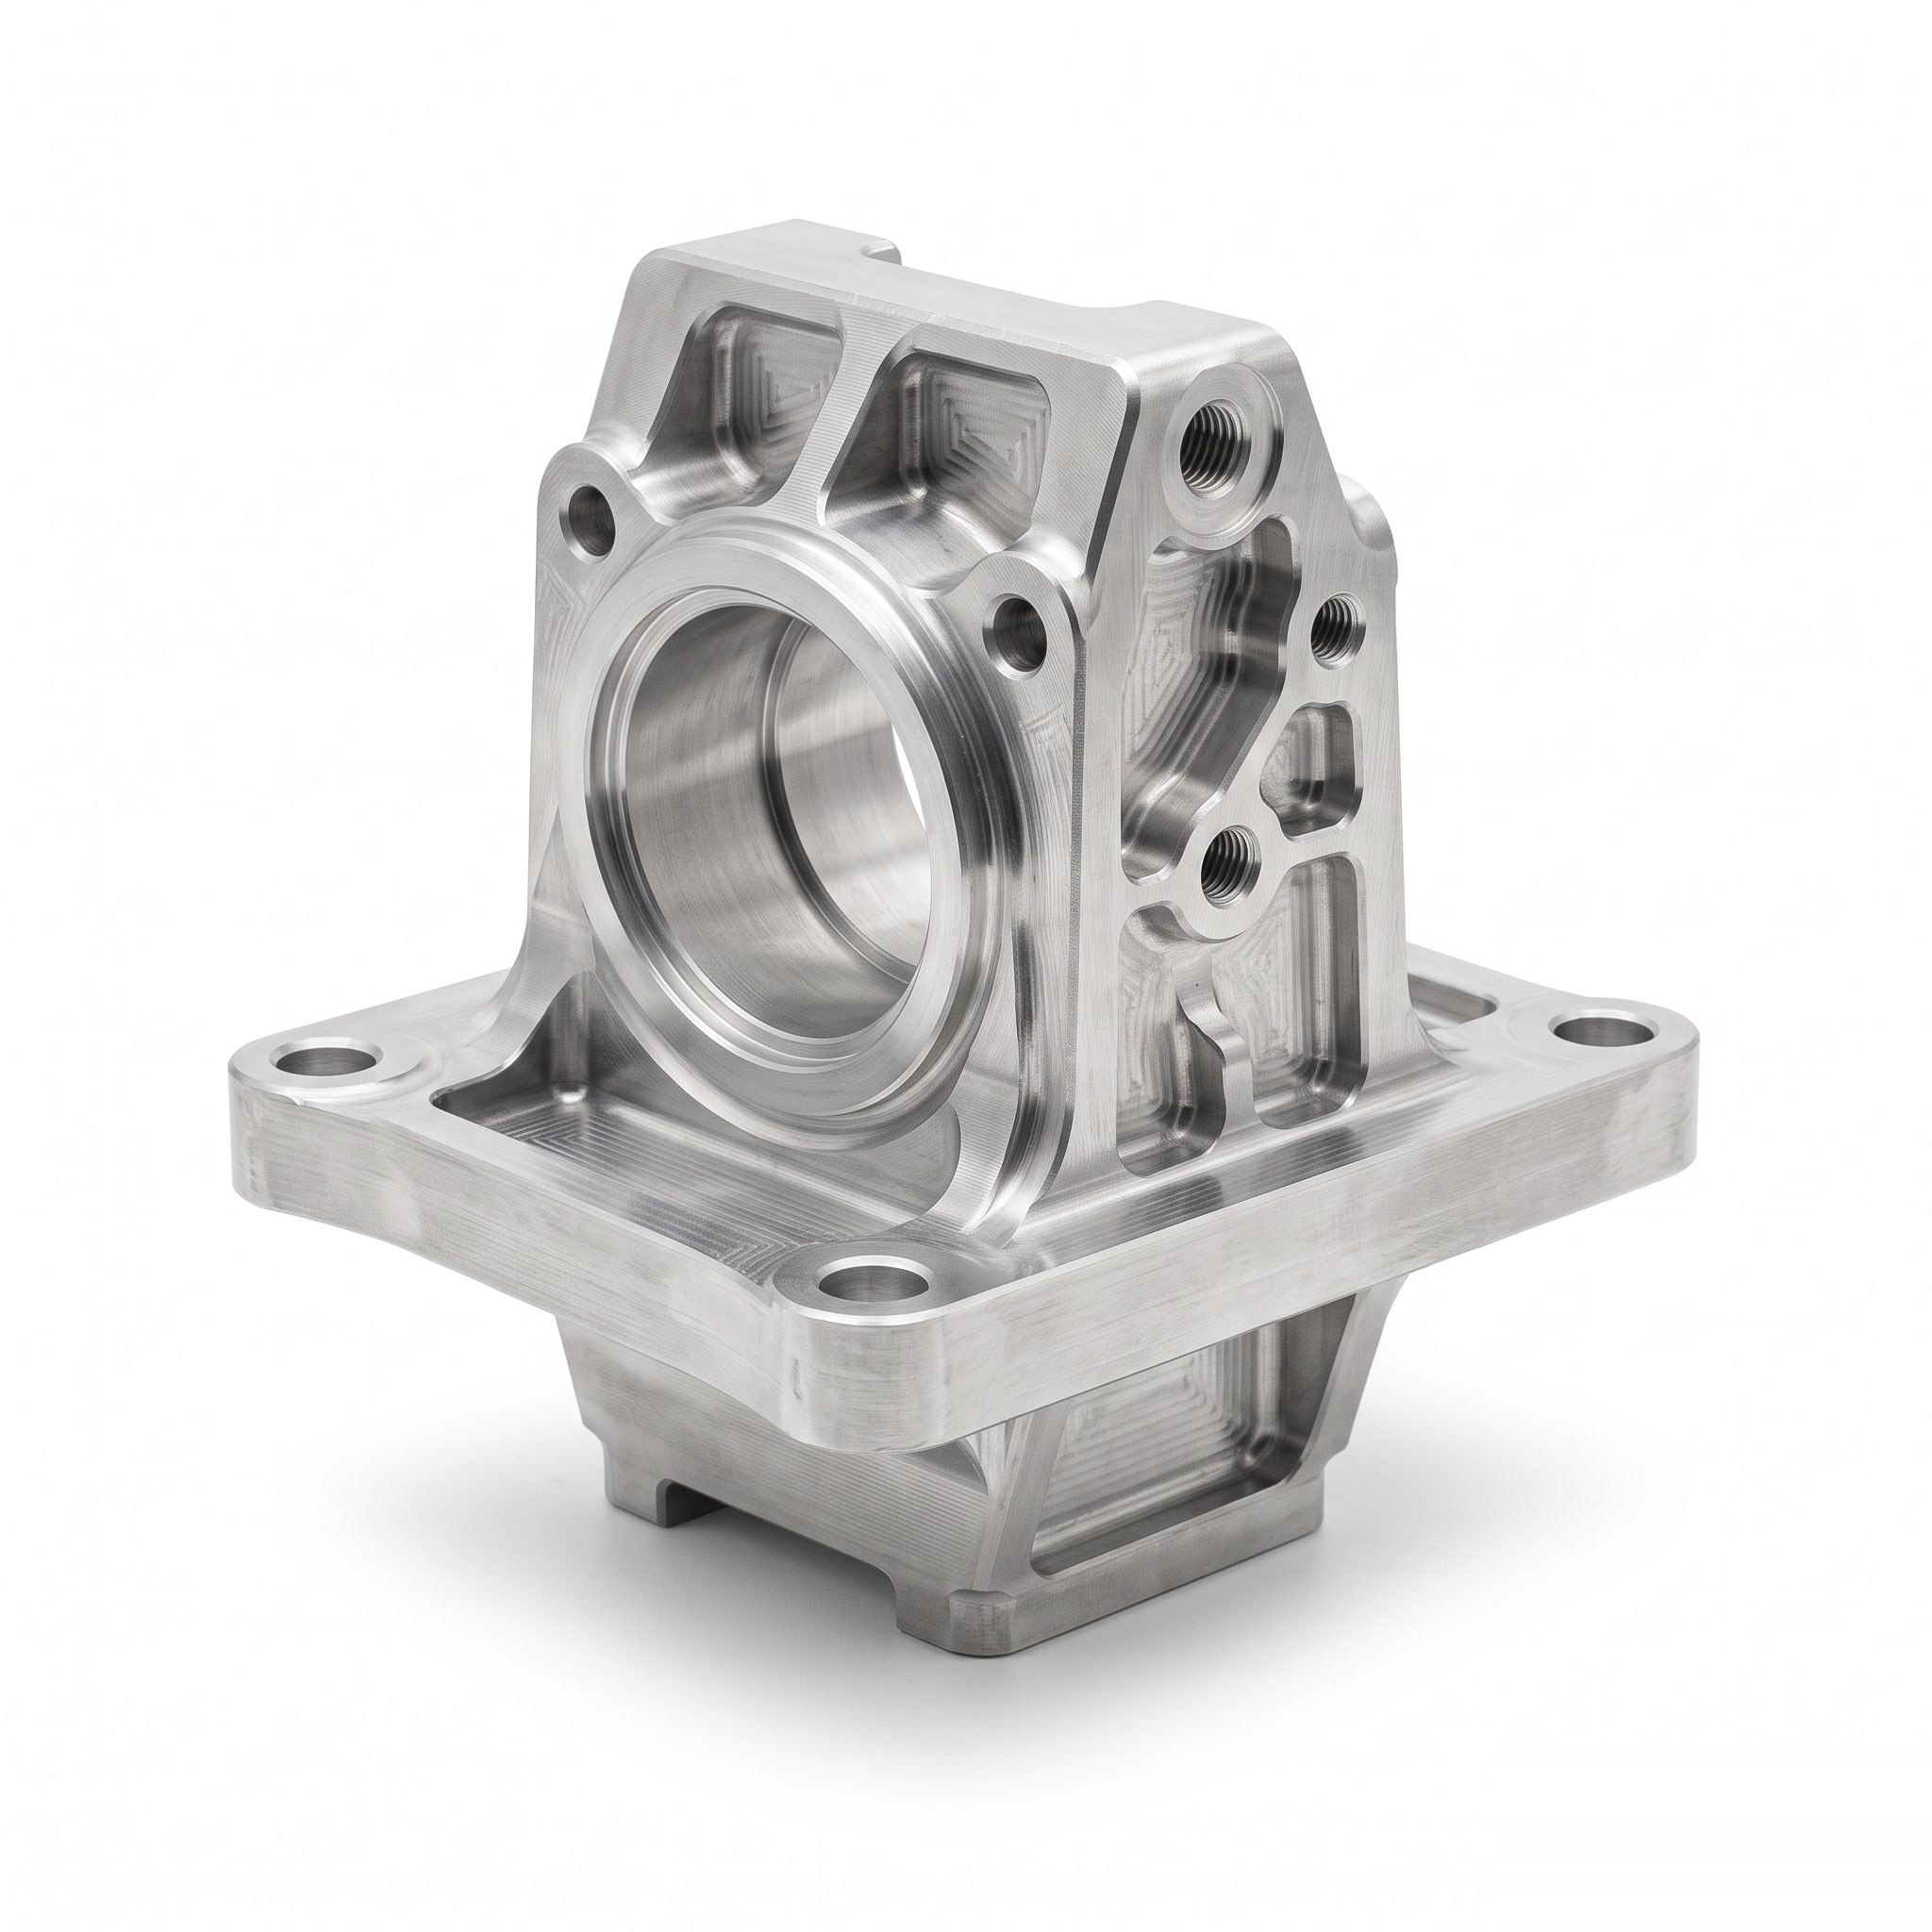
Custom steering base housings with a large circular bore, reinforcing ribs and a mounting flange for the interfaces specified by the steering assembly design.
View Details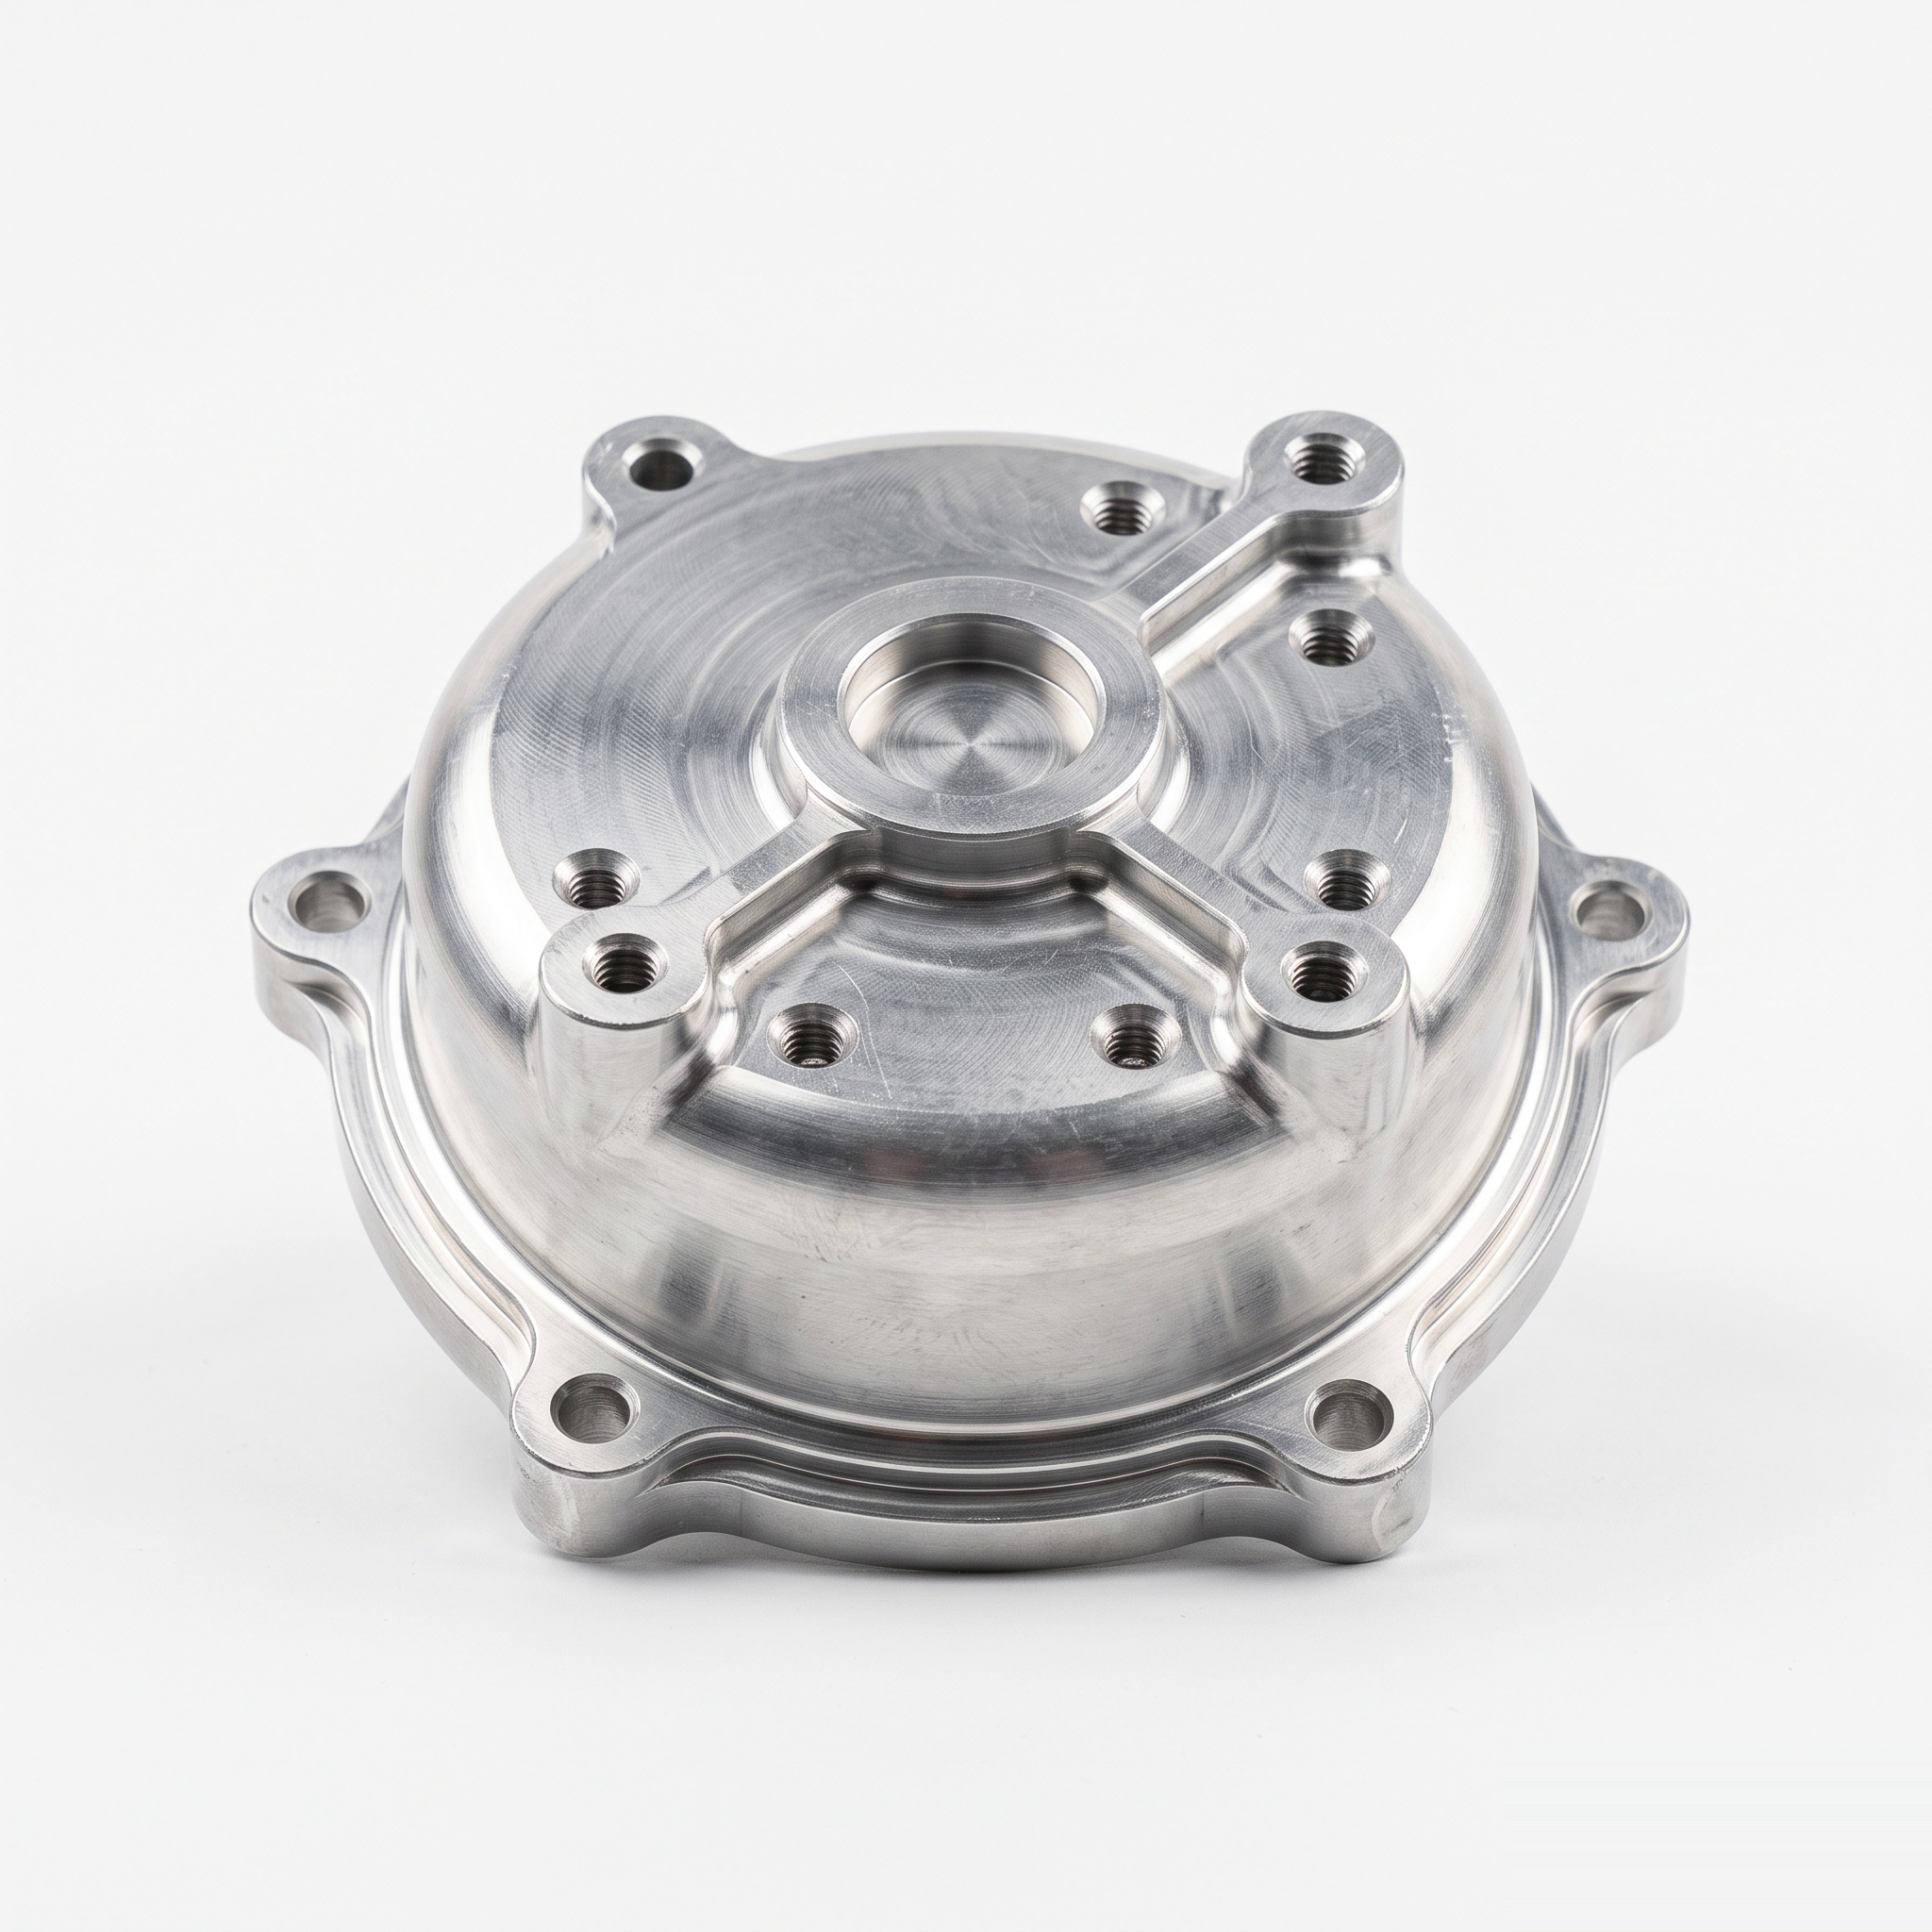
Steering Covers
Steering assembly covers with a raised central section, circular mounting flange and fixing holes, customized to the required internal clearance and housing interface.
View Details
Mounting Retainer Plates
Formed mounting and retainer plates with a large opening, locating tabs and fixing holes for customer-designed retention and installation arrangements.
View Details